Tag Archives: CrossFire XR

Pierce Height vs Cut Height: Why CNC Plasma Uses Two Different Heights

Pierce height vs Cut Height

Pierce Height vs Cut Height: Why CNC Plasma Uses Two Different Heights One of the easiest CNC plasma settings to misunderstand is torch height. The torch does not stay at one fixed distance above the material throughout the entire cutting process. Instead, a typical plasma cut uses two important heights: Pierce height Cut height They […]
How the Floating Z-Axis Sets Torch Height on a CNC Plasma Table

Floating Z axis

How the Floating Z-Axis Sets Torch Height on a CNC Plasma Table Before a CNC plasma cutter can make a good cut, it needs to know exactly where the surface of the material is. That sounds simple until you consider that sheet metal is rarely perfectly flat. Material can be: Warped Bowed Sitting unevenly on […]

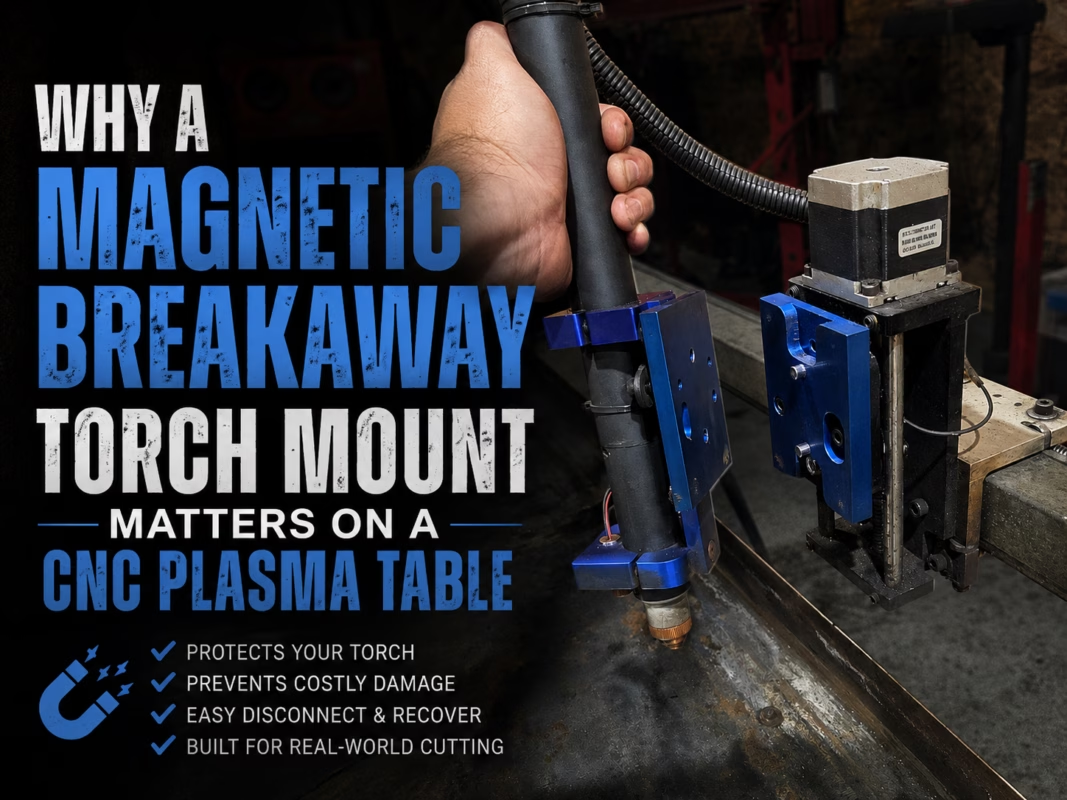
Why a Magnetic Breakaway Torch Mount Matters on a CNC Plasma Table

Magnetic Torch Mount

Why a Magnetic Breakaway Torch Mount Matters on a CNC Plasma Table Even with a properly set up CNC plasma table, eventually something is going to go wrong. A cut part tips up. A piece of warped material catches the torch. Slag builds up. A remnant moves. The torch travels across something that is no […]

Why Torch Lead Routing Matters on a CNC Plasma Table

Torch Lead Routing Matters

Why Torch Lead Routing Matters on a CNC Plasma Table The torch lead is easy to overlook when setting up a CNC plasma table. It is flexible, so it may seem like you can simply route it wherever it fits and start cutting. But that heavy cable is constantly pulling on the torch as the […]