
 Beck’s Toolbox
 Knives
 DIY Build Kits
 Digital Downloads
 Machine Accessories
 Fabricating Materials
CNC Plasma Cutting
Why CNC Plasma Small Holes Cut Poorly and How to Improve Them
Oct
Why CNC Plasma Small Holes Cut Poorly and How to Improve Them
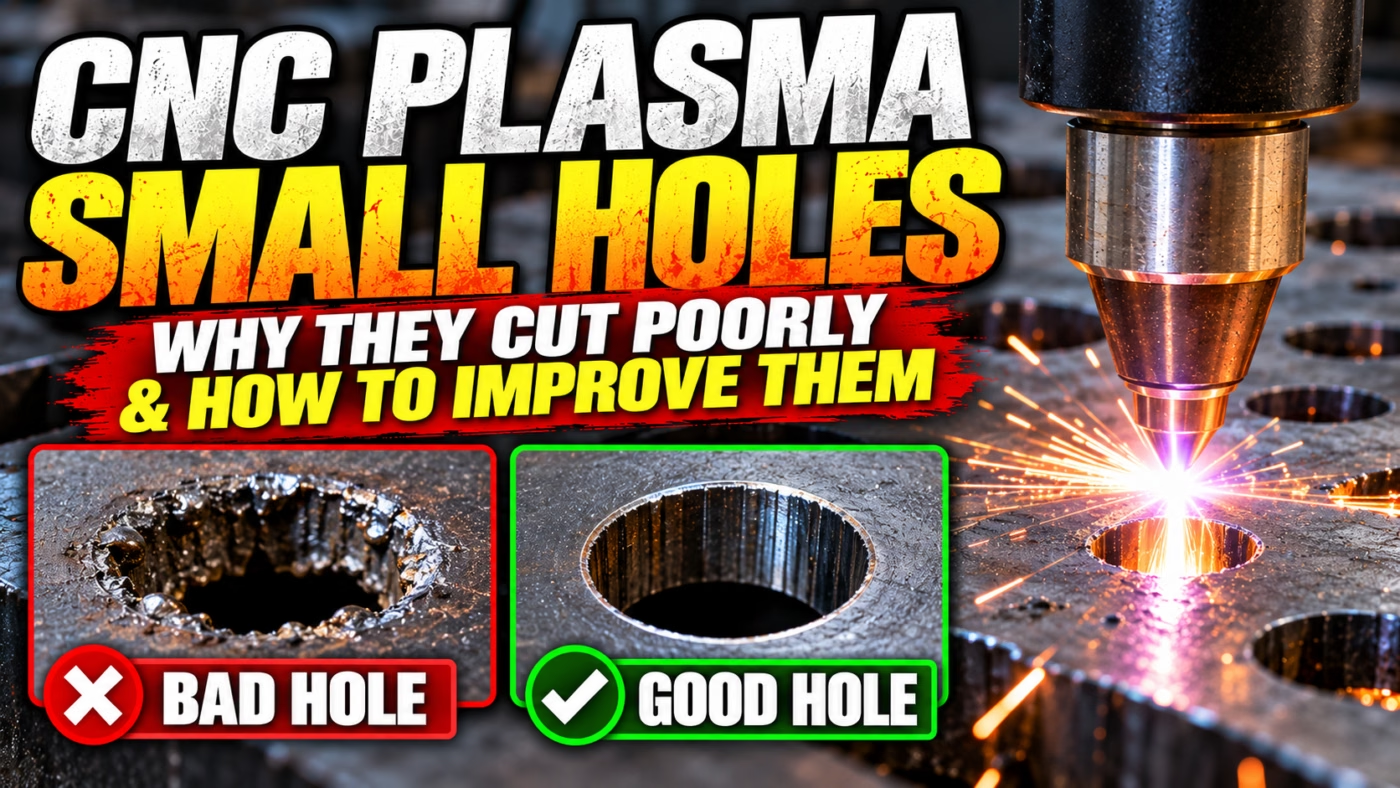
CNC plasma cutters can produce surprisingly accurate parts, but small holes are one area where things can get frustrating fast.
You draw a 1/4-inch hole in CAD.
The machine cuts it.
Then you grab a 1/4-inch bolt and it won’t go through.
Or the top of the hole looks reasonably round while the bottom is tapered, ugly, or full of dross.
This doesn’t necessarily mean your plasma table is inaccurate.
Small holes are simply much more demanding than cutting a large outside profile.
Why Small Holes Are Harder to Plasma Cut
A plasma arc is not a perfectly straight cylindrical cutting tool.
It has width, shape, direction, and some degree of taper.
When cutting a large profile, those characteristics are spread over a relatively long toolpath.
A small hole forces the machine to change direction constantly while maintaining:
- Correct torch height
- Correct cutting speed
- Stable arc voltage
- Proper kerf compensation
- Smooth circular motion
The smaller the hole becomes relative to the material thickness, the less forgiving the process becomes.
Cutting Speed Is One of the Biggest Factors
Your normal straight-line cutting speed may be too fast for a small hole.
The machine has to continuously accelerate and change direction while moving around a tight circle.
Even if your program commands 100 IPM, the machine may never actually reach 100 IPM before it has to begin changing direction again.
That changes what the plasma arc is doing compared with a long straight cut.
For this reason, many plasma-cutting strategies reduce speed when cutting small holes.
But slower is not automatically better.
Slow down too much and you can create excessive heat, a wider kerf, and heavy low-speed dross.
The goal is a controlled reduction in speed rather than simply crawling around the hole.
Kerf Compensation Matters Even More on Small Features
Imagine having a kerf width of 0.060 inch.
On a 12-inch plate, that 0.060-inch kerf is relatively small compared with the overall part.
On a 0.250-inch hole, it is huge.
That means even a small error in kerf compensation can make a noticeable difference in the finished diameter.
This is why I recommend measuring the actual kerf produced by your machine rather than blindly relying on a default value in your CAM software.
Your kerf can change with:
- Material thickness
- Amperage
- Consumable size
- Cutting speed
- Torch height
- Consumable wear
Get the cutting process stable first, then dial in your kerf compensation.
Lead-Ins Can Ruin a Small Hole
Every plasma cut needs to start somewhere.
On an outside profile, you usually have plenty of scrap material available for a lead-in.
A small hole gives you very little room.
A poorly positioned lead-in can leave a divot, gouge, or oversized area where the arc transitions into the finished circle.
The smaller the hole, the more important your lead-in strategy becomes.
You want the pierce and transition to occur without damaging the finished edge.
Depending on your CAM software and hole size, a short lead-in or specialized small-hole strategy may work better than the same lead-in you use for larger profiles.
Lead-Outs Can Cause Problems Too
It is easy to focus on where the cut starts and ignore where it stops.
If the torch continues moving after completing the circle, the arc can cross back into the finished edge.
This can leave a notch or oversized area.
In some situations, stopping the cut at the correct point without a traditional lead-out can produce a better hole.
Again, this depends on your CAM software, plasma cutter, material, and hole size.
Small-hole cutting usually requires different thinking than a normal outside contour.
Torch Squareness Becomes Very Important
A crooked torch can sometimes be difficult to notice on large outside profiles.
Small holes make the problem much more obvious.
If the torch is not perpendicular to the material, one side of the hole can taper differently than the other.
Before spending hours adjusting CAM settings, make sure your Z-axis and torch are actually square.
See Why CNC Plasma Torch Squareness Matters for Cut Quality.
The torch also needs to remain rigidly and repeatably positioned. The [Beck Tools Machine Torch Holder] product page uses full-radius clamping to securely support compatible machine torches rather than relying on a traditional V-block arrangement.
Torch Height Has to Stay Consistent
Small holes do not give the THC much time to react.
Depending on your controller and cutting strategy, aggressive THC correction during a tiny circular cut can actually create more problems than it solves.
This is especially true if something else is changing the arc voltage.
Air-pressure changes, poor lead routing, warped material, or mechanical movement can all affect what the THC sees.
Make sure your floating Z-axis is functioning correctly and your torch lead has enough controlled slack throughout the machine’s travel.
Read Why Torch Lead Routing Matters on a CNC Plasma Table.
Worn Consumables Show Up Quickly in Small Holes
A nozzle with a damaged or enlarged orifice changes the shape of the plasma arc.
You might still get acceptable results cutting large brackets or rough profiles.
Small holes are much less forgiving.
If hole quality suddenly gets worse, inspect your nozzle and electrode before rewriting your program.
You can spend a lot of time trying to compensate in software for a worn piece of copper.
Tipped Parts and Torch Crashes Can Destroy Your Setup
Small holes are often only one feature in a much larger nested sheet.
That means your torch still has to travel around previously cut parts, scrap, and potentially tipped pieces.
A collision can knock the torch out of alignment and immediately change your hole quality.
The [Beck Tools Magnetic Breakaway Torch Mount] product page is designed to allow the torch-holder assembly to release during a significant collision rather than transferring the entire impact into the torch and Z-axis.
It does not replace proper THC settings or good cut sequencing, but it adds protection when something unexpected happens.
You can also read Why a Magnetic Breakaway Torch Mount Matters on a CNC Plasma Table.
Sometimes the Best Plasma-Cut Hole Is a Pilot Hole
There is a point where trying to produce a finished precision hole directly with plasma stops making sense.
If I need an accurate hole for:
- A dowel pin
- A close-fit bolt
- A bearing
- A shaft
- A precision locating feature
I would rather plasma cut a smaller pilot hole and finish it mechanically.
That might mean drilling, reaming, boring, or machining it later.
Trying to make a plasma cutter hold machining tolerances usually creates more work than simply choosing the correct manufacturing process.
The plasma cutter is still doing the valuable work because it quickly establishes the hole location and removes most of the material.
A Practical Small-Hole Troubleshooting Order
If your holes are coming out poorly, I would troubleshoot them in this order:
- Inspect the electrode and nozzle.
- Verify torch squareness.
- Verify cut height.
- Confirm your kerf value.
- Check your lead-in and lead-out.
- Reduce hole-cutting speed in controlled increments.
- Check airflow and THC behavior.
- Cut another test part and measure it.
Only change one or two variables at a time.
Otherwise, you will eventually get a good hole without knowing which change actually fixed it.
The Bottom Line
Small holes expose problems that larger plasma-cut profiles can hide.
Kerf error, torch misalignment, worn consumables, incorrect speed, poor lead-ins, and unstable torch height all become much more noticeable as the diameter gets smaller.
Start with a mechanically sound machine and good consumables.
Then work on your cutting strategy.
And remember that not every hole needs to come off the plasma table completely finished.
Sometimes the best solution is using the plasma cutter for what it does well and finishing critical features with the correct secondary operation.
For more practical CNC plasma setup and troubleshooting articles, visit the Beck Tools Guides.
Category: CNC Plasma Cutting
Tags: CNC Plasma, Small Holes, Plasma Hole Quality, Kerf Compensation, CNC Plasma Accuracy, Torch Height, Plasma Consumables, CNC Plasma Troubleshooting
